
Seven common construction methods for blast furnace iron tapping channels
author: XINTAI
2025-07-02

1. Pounding and shaping method
This method was the previous construction approach for the inner lining of the iron tapping channel, often used on the iron tapping channel of small blast furnaces. It has gradually evolved from manual ramming or pneumatic hammer ramming and on-site mechanical compaction in the 1970s to automatic ramming with an automatic hammer suitable for different parts.
This method was the previous construction approach for the inner lining of the iron tapping channel, often used on the iron tapping channel of small blast furnaces. It has gradually evolved from manual ramming or pneumatic hammer ramming and on-site mechanical compaction in the 1970s to automatic ramming with an automatic hammer suitable for different parts.
2. Casting construction method (N-Cast method)
In the late 1970s, Japan developed the pouring construction method. This method involves inserting a vibrator into the trench material for direct vibration, as the trench material contains a relatively high amount of moisture. This method has several major advantages:
(1) Some residual linings can be retained to enhance the utilization rate of lining materials.
(2) The trench lining has uniform structure, low porosity and good durability.
(3) It has reduced the labor intensity of workers and improved the on-site construction environment. The disadvantages are that it is noisy and the drying time is relatively long.
3. Core mold vibration forming Method (VF method
The groove material poured into the iron groove is placed into an inner mold equipped with a vibrator. While vibrating at a frequency of several thousand Hertz and applying pressure, the thixotropy of the low-moisture groove material is utilized to promote the flow and densification of the refractory material. The forming mold gradually sinks to form the desired groove shape. The proportion of water in the gutter used in this method is 4% to 6%. Compared with the ramming method, this method is more efficient, consumes less refractory materials, and improves the quality of the iron tapping groove. However, the compactness of the groove lining on the side close to the permanent layer is poorer than that on the side close to the inner mold.
4. Core mold dry Vibration forming Method (SVP method
The construction machinery for the dry vibration forming method of core mold is relatively complex. The inner formwork is equipped with high, medium and low-frequency vibrators. After being placed in position, it vibrates while adding materials to build the trench lining [7]. This method uses dry materials for vibration molding, which can be dried quickly without cracking, saving time. It is particularly suitable for the use of single iron outlet fixed grooves. In addition, the absence of moisture can reduce porosity and increase density, which can extend the service life of the iron channel.
5. Large brick and prefabricated component masonry method
Iron groove prefabricated parts are cast and formed in prefabricated molds according to the shape and size of the iron groove. At present, this method is developing rapidly. It involves completing all the processes such as molding, drying, curing and baking in the refractory materials factory. The masonry is also relatively fast and can be put into use immediately after production. It is very suitable for iron water channels and spout parts. Its advantages are that it can be pre-baked, is not limited by the iron tapping time, and can ensure that the performance of the castable is not restricted by the construction conditions, thereby obtaining high-strength iron channel material and relatively extending the service life of the iron tapping channel. Its drawback is that the external dimensions cannot be too large; otherwise, the baking conditions cannot meet the requirements. Another drawback is that when used in the iron groove, the seams existing between the prefabricated components become the weak link in the iron groove.
6. Self-flowing casting
Since France developed self-flowing castable, Japan has studied self-flowing iron channel castable. It does not require vibration during construction. Relying on the self-weight and position difference of the material, the castable can generate self-flow to achieve degassing, leveling and compactness. It is a viscoplastic material with a relatively low yield value and certain plastic viscosity, developed based on rheological principles. Its advantages are:
(1) It does not require vibration and can automatically pour densely, greatly reducing the labor intensity.
(2) If the pumping process is adopted during construction, it will reduce labor and improve efficiency;
(3) It has stronger adaptability than vibrating castable materials and can be cast into any shape.
7. Iron groove repair method
The lining of the slag line and molten iron line in the iron tapping channel of the blast furnace is damaged relatively quickly, especially when the ratio of slag to iron is relatively high. For this purpose, hot spray repair materials can be used to repair the trench lining, achieving balanced damage and thereby increasing its service life. The refractory spray repair materials used in the iron tapping channel of blast furnaces generally adopt high aluminum-silicon carbide, Al2O3-SiC-C and mullite-silicon carbide materials. The patching of the iron tapping channel in a blast furnace is generally carried out after the iron tapping has been completed and the residual iron in the lining has been removed. Spray repair can be started when the temperature is between 400 and 900 degrees Celsius, or it can be carried out at room temperature. Each time a spray repair is carried out, the thickness of the spray repair layer is 70 to 150mm. The disadvantages are that the rebound loss of the spray coating material is large, it is not dense enough and it is prone to delamination.
The design and selection of refractory materials for the bottom and interior of non-ferrous metal smelting furnaces
The development and changes of the materials for the iron tapping ditch
Related Article

Refractory materials are the main building materials of glass melting furnaces, and they have a decisive impact on the quality of glass, energy consumption and even product costs. The development of glass melting technology largely depends on the advancement of refractory material manufacturing technology and the improvement of quality.
Selection of kiln type structure and lining refractory materials for glass melting furnaces
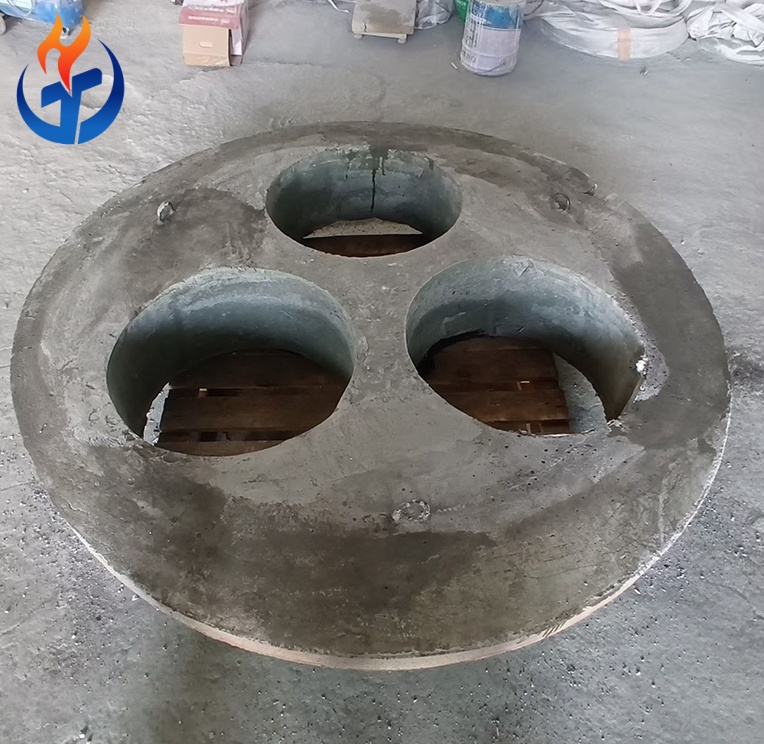
The cover of the electric furnace is a spherical structure with electrode holes and smoke exhaust holes. The outer ring part is called the main furnace cover, and the middle part is called the small furnace cover (also known as the triangular area). When loading materials, the furnace cover can be moved away.
Factors affecting the service life of refractory materials used for electric furnace covers
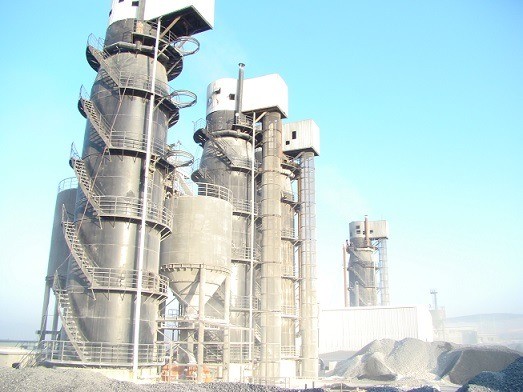
Overburning and lumping are common phenomena in the lime production process. They not only affect product quality but, in severe cases, can have a fatal impact on the production process, refractory materials of the kiln body and other equipment. This article analyzes the causes of overburning and tumor formation, general treatment methods for tumor formation, and preventive measures, effectively avoiding the occurrence of tumor formation.
Common causes of lumps in lime kilns and their solutions

A kiln is a space capable of generating high temperatures, and the materials that make up this space are called kiln construction materials. The construction materials should include two major categories: refractory materials and thermal insulation materials (or heat insulation materials). In addition, to enhance the structural strength of the kiln body, the materials used for furnace construction should also include common building materials (such as ash bricks, etc.) and metal materials, etc.
Don't know how to build a kiln or furnace? This article is enough