
How to construct refractory castables that have been stored for a long time
author: XINTAI
2025-09-11

1. Mixing Refractory Castables
The mixer and other equipment must be clean before use. Any debris may significantly affect the performance of the castable. The mixing water must be clean. At room temperature, to reduce excessive evaporation and excessive temperature rise, avoid excessive ventilation, heating, and direct sunlight during the mixing process. In lower temperatures, appropriate heating should be applied to prevent the material from freezing. Concrete must be mixed using a forced mixer to reduce the water content and improve mixing quality. Adding water to improve the pourability of a partially set mixture is not permitted; this will cause the castable to lose significant strength.
The mixer and other equipment must be clean before use. Any debris may significantly affect the performance of the castable. The mixing water must be clean. At room temperature, to reduce excessive evaporation and excessive temperature rise, avoid excessive ventilation, heating, and direct sunlight during the mixing process. In lower temperatures, appropriate heating should be applied to prevent the material from freezing. Concrete must be mixed using a forced mixer to reduce the water content and improve mixing quality. Adding water to improve the pourability of a partially set mixture is not permitted; this will cause the castable to lose significant strength.
To ensure uniform mixing and minimize the water content, ensuring high strength and uniformity of the castable, the castable must be mixed dry for 1 minute. 50% of the water should be added and mixing continued for 1 minute. The remaining water should then be added gradually as needed, aiming for an optimum value between 80% and 100% of the required water content. Mixing time should be based on the manufacturer's specifications. After adding water, the mixing time should be approximately 5 minutes. The amount of water added should be minimized. Excessive mixing water will cause bleeding and segregation between the slurry and aggregate, resulting in slurry loss and a significant reduction in masonry strength. The amount of castable material mixed each time should be an integer multiple of the minimum batch size, i.e., 100-300 kg.
The appropriate amount of water added can be verified using the following method. After adding water and mixing, it will reach a certain consistency in about 4 minutes. At this point, you can form a concrete ball in one hand. After squeezing it 5-6 times with your fingers together and then opening your palm, it will lose its shape and slowly spread out in your palm. The amount of water added should be appropriate so that it does not flow through your open fingers. Pour the mixed castable into the formwork and continuously vibrate it from the bottom until all air is expelled and the castable is uniform and integrated. However, do not overdo this process, which may cause surface bleeding or slurry segregation. Prolonged vibration can also cause the refractory steel fibers to become arranged in a disordered manner within the castable (resulting in a chaotic and disorganized image), thereby reducing the anti-stripping properties of the refractory fibers within the castable.
Casting within the zones separated by expansion joints must be poured continuously in a single pass. Casting should be continuously added and vibrated until the formwork is completely filled. Pouring should not be paused until the designated zones are complete. Pouring and vibration must be completed before any portion of the castable within the zone begins to set. Layered pouring should be avoided as much as possible. If partial layer pouring is not possible, the second layer must be poured before the first layer sets. Applying castable over already solidified castable is pointless and will fall off at low temperatures. During vibration, the castable surface will tend to level out. If a special shape is required, the vibrator can be moved parallel to the desired surface to push the material in the desired direction.
2. Hardening and Curing of Castables
After the castable begins to set, it must harden for at least 24 hours at room temperature. Extending the hardening time to 48 hours or longer can, to some extent, improve concrete strength. Low-cement castables often require longer setting times. Curing and demolding times should be appropriately extended for areas where high-strength castables are used, such as coal injection pipes and kiln openings. Before hardening, moisture evaporation should be prevented. This can be achieved by covering the lining with a thin layer of plastic or grass matting, or by applying mud and water. During this period, due to the low strength of the concrete, excessive mechanical forces that could damage the concrete should be avoided.
After the castable begins to set, it must harden for at least 24 hours at room temperature. Extending the hardening time to 48 hours or longer can, to some extent, improve concrete strength. Low-cement castables often require longer setting times. Curing and demolding times should be appropriately extended for areas where high-strength castables are used, such as coal injection pipes and kiln openings. Before hardening, moisture evaporation should be prevented. This can be achieved by covering the lining with a thin layer of plastic or grass matting, or by applying mud and water. During this period, due to the low strength of the concrete, excessive mechanical forces that could damage the concrete should be avoided.
After hardening, the castable should be allowed to dry for a period of 24 to 48 hours at an ambient temperature of 15 to 30°C. The lower the temperature, the longer the hardening time. If the temperature drops below 10°C, consider increasing the temperature to improve curing conditions. Sodium silicate and phosphate castables should be cured in a dry environment to utilize the dehydration of the sodium silicate to increase strength. Avoid watering during curing.
The demolding time should be appropriately chosen: Non-load-bearing formwork should be demolded when the castable strength is sufficient to prevent it from falling off due to cold. Load-bearing castables should be demolded when their strength reaches 70%. High-strength core forms should be demolded promptly before concrete damage occurs, to avoid difficulties with demolding due to excessive castable strength.

3. Drying and Heating of the Preheater and Precalciner Systems
After hardening or drying, the castable still contains residual physical and chemical water. Heating to 300°C will vaporize and dehydrate it, completely draining away all the water. Due to the dense structure of the castable, the heating rate must be slow to avoid damage caused by stress generated by the rapid temperature increase and excessive evaporation of water.
After hardening or drying, the castable still contains residual physical and chemical water. Heating to 300°C will vaporize and dehydrate it, completely draining away all the water. Due to the dense structure of the castable, the heating rate must be slow to avoid damage caused by stress generated by the rapid temperature increase and excessive evaporation of water.
The kiln system's drying and heating schedule may not always meet the drying requirements of the preheater and precalciner (the grate cooler, kiln head hood, and tertiary air duct meet the kiln system's drying and heating schedule and are not listed separately). Therefore, the kiln system's baking and heating schedule, described below, should be implemented in conjunction with the requirements of this section. If the primary preheater fails to meet the drying requirements when the kiln system reaches 600°C (based on the kiln exhaust gas temperature), the kiln system's holding time at 600°C should be extended.
The final batch of refractory castables should be cured at a temperature of approximately 25°C for at least 24 hours (for low-cement castables, the curing time should be extended to 48 hours, if appropriate). Once the castables have achieved a certain strength, the formwork and supports are removed, and after 24 hours of drying, they can be baked out. If the curing temperature is too low, the curing time may need to be extended. Based on the kiln exhaust gas temperature, the temperature should be increased at a rate of 15°C/hour until it reaches 200°C, holding for 12 hours. The temperature should then be increased at a rate of 25°C/hour to 400°C, holding for at least 6 hours. The temperature should then be increased to 600°C, holding for at least 6 hours.
The following two conditions are necessary and sufficient for the bakeout of the decomposition furnace and preheater systems: When the temperature of the refractory castable at the cyclone preheater pouring hole, on the side closest to the silicon cover plate, reaches 100°C, the drying should continue for at least 24 hours. At the manhole door of the first-stage cyclone preheater, a clean piece of glass was used to contact the flue gas, and no water vapor leakage on the glass was observed. After keeping warm for 6 hours.
4. Castable Maintenance
After hardening or drying, castables still contain residual physical and chemical water. Heating to 300°C will vaporize and dehydrate them, completely draining out the water. Due to the dense structure of castables, the heating rate must be slow to avoid damage caused by stress due to rapid temperature increases and excessive evaporation of water.
After hardening or drying, castables still contain residual physical and chemical water. Heating to 300°C will vaporize and dehydrate them, completely draining out the water. Due to the dense structure of castables, the heating rate must be slow to avoid damage caused by stress due to rapid temperature increases and excessive evaporation of water.
The kiln system's drying and heating schedule may not always meet the drying requirements of the preheater and decomposition furnace (the grate cooler, kiln head hood, and tertiary air duct meet the kiln system's drying and heating schedule and are not listed separately). Therefore, the kiln system's baking and heating schedule, described below, should be implemented in conjunction with the requirements of this section. If the primary preheater fails to meet the drying requirements when the kiln system reaches 600°C (based on the kiln exhaust gas temperature), the kiln system's holding time at 600°C should be extended.
The final batch of refractory castables should be cured at a temperature of approximately 25°C for at least 24 hours (for low-cement castables, the curing time should be extended to 48 hours, if appropriate). Once the castables have achieved a certain strength, the formwork and supports are removed, and after 24 hours of drying, they can be baked out. If the curing temperature is too low, the curing time may need to be extended. Based on the kiln exhaust gas temperature, the temperature should be increased at a rate of 15°C/hour until it reaches 200°C, holding for 12 hours. The temperature should then be increased at a rate of 25°C/hour to 400°C, holding for at least 6 hours. The temperature should then be increased to 600°C, holding for at least 6 hours.
The following two conditions are necessary and sufficient for the bakeout of the decomposition furnace and preheater systems: When the temperature of the refractory castable at the cyclone preheater pouring hole, on the side closest to the silicon cover plate, reaches 100°C, the drying should continue for at least 24 hours. At the manhole door of the first-stage cyclone preheater, a clean piece of glass was used to contact the flue gas, and no water vapor leakage on the glass was observed. After keeping warm for 6 hours.
Beyond the Price Tag: The Hidden Costs of Choosing the Wrong Unshaped Refractory
Composition and properties of ramming material for glass kiln
Related Article
Why smart engineers look at total cost of ownership, not just unit price, when selecting monolithic refractory materials
Beyond the Price Tag: The Hidden Costs of Choosing the Wrong Unshaped Refractory
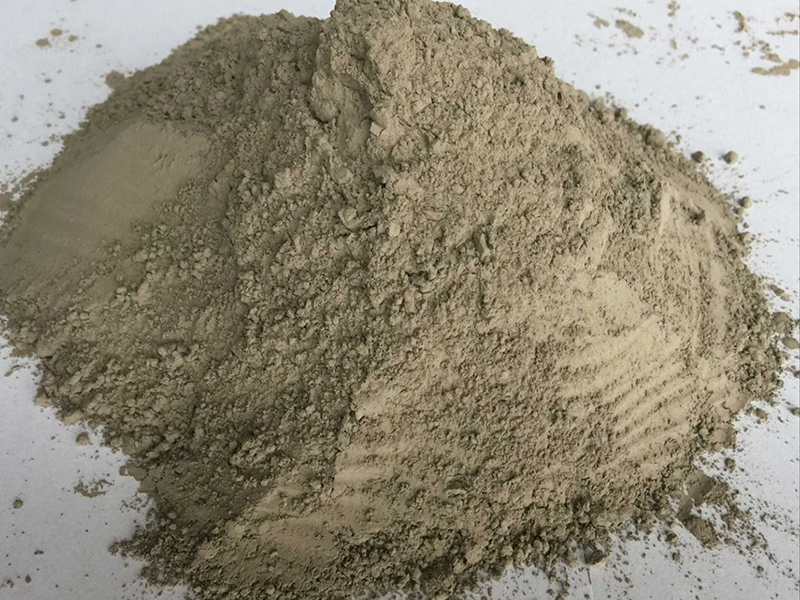
Henan Xintai Refractory Materials Co., Ltd. manufactures monolithic refractory materials that are constructed using ramming (manual or mechanical) and hardened by heating above room temperature. These materials are composed of graded refractory aggregate, powder, binder, and admixtures, mixed with water or other liquids. Ramming materials include high-alumina, clay, magnesia, dolomite, and zirconium.
Composition and properties of ramming material for glass kiln

There are many factors that affect the rheological properties of castable materials, such as the limit size, shape, distribution and water absorption rate of particles; the properties and dosage of binders and dispersants, the amount of water added, and the mixing and stirring process, etc. However, the most significant influences are the bonding system, particle size distribution and the properties and dosage of dispersants.
Five main factors affecting the rheological properties of refractory castables

Admixtures are substances that, when added in appropriate amounts to the batching of refractory materials, can improve the physical properties, formability or construction performance, and service performance of refractory materials. They are also known as additives.
Common admixtures for unshaped refractory materials